
Laser safety in Australia is regulated by
AS-60825, “Safety of laser products”
Updated 6 April 2026 by Neil Silke.
SCOPE: This article covers industrial lasers, not medical or cosmetic lasers. Medical or cosmetic lasers are different and require the operator to be registered in some states, such as Tasmania, Queensland and Western Australia, but this article is not aimed at or authoritative on medical and cosmetic lasers.
So far as I can find, Western Autralia is the only state that requires registration of workplace lasers, via the Radiological Council in W.A. This is detailed at the end of this section.
The standards for industrial laser welders and cleaners are well established. Australia, New Zealand and most of the world has adopted the European laser safety and machinery standards as discussed in this article. These standards were established at least ten years ago and are accepted as safe.
Most Australian Standards are not actually legislated. However the standards could be legislated in the future, and either way it is foolish not to follow them. By following the relevant set of Australian Standards, in the event of an incident you can demonstrate that you did all things reasonably possible to manage your risk. And, of course, the risk of an accident is greatly reduced if you follow Australian Standards in your workplace. AS/NZS 60825 recommends that a workplace has a designated Laser Safety Officer. This would normally be your OH&S person, after doing a laser safety training course such as an on-line course. Online courses are usually very broad so, in addition, they should read this and other articles on laser safety to get a practical understanding of the hazards and recommendations for laser welding and cleaning.
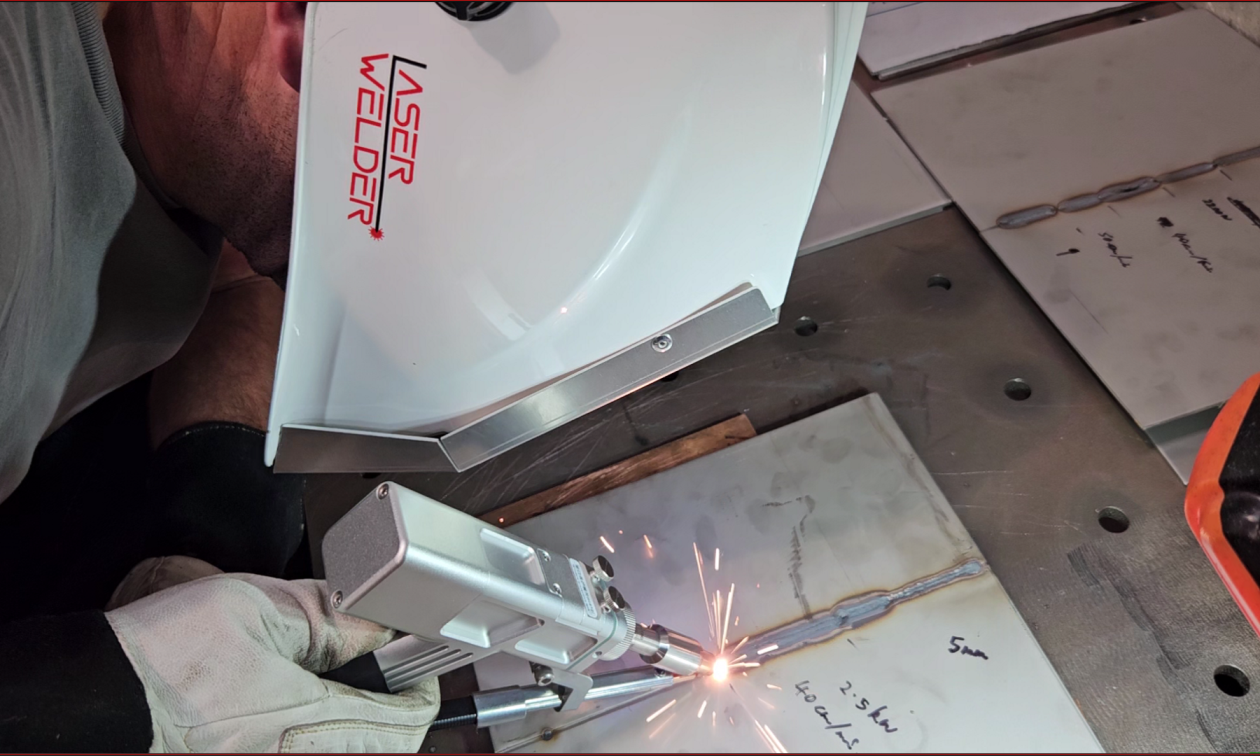
As stated in AS-60825, hand held laser welders and cleaners are class 4 devices, meaning exposure to them can cause eye and skin damage. They can also start fires close to the laser handpiece where the intensity is high. DESPITE the videos you may see of people using them without eye protection, lasers MUST be treated with respect and the proper precautions must be taken. This is especially true because the laser light is invisible, so there is zero warning that laser light is present. Our laser welders focus the beam at the welding zone, and the beam then diverges, becoming less intense as it moves away from the welding handpiece. To illustrate the risk: Our calculations show the laser intensity is high enough to damage eyes up to 130m away, if not enclosed.
It is interesting to understand where the legal requirements come from. From an Australian federal legislative framework and legal perspective Safe Work Australia (safeworkaustralia.gov.au) is the government body that monitors and tries to improve workplace safety. They work with the Australian Standards committees, who decide what standards should be adopted, and if necessary would ask the relevant minister to make certain standards legislated (legally mandatory).
State Legislation is usually found in the published rules of each State Government’s OH&S (occupational health and safety) department. These rules are generally high level, requiring the company or owner to create a safe environment and avoid workers being exposed to injury. They may or may not reference an Australian Standard directly.
Note that Safe Work Australia prohibits Class 4 (and Class 3b) lasers for building and construction, because the environment is not controlled. However industrial uses such as metal fabrication in controlled, enclosed areas are allowed.
For detailed laser safety requirements, Safe Work Australian directs us to another government body, ARPANSA (Australian Radiation Protection and Nuclear Safety Association). As of 22 February 2026, ARPANSA says “Lasers are classified according to the hazard associated with their emissions, as defined in the Australian/New Zealand Standard AS/NZS IEC 60825.1:2014 Safety of Laser Products Part 1: Equipment classification and requirements, AS/NZS IEC 60825.14:2011 Safety of Laser Products Part 14: A User’s guide.”
ARPANSA also says the following safety eyewear standards are to be followed:
“The Australian standard AS/NZS 1337.4:2011 Eye and face protection Part 4: Filters and eye protectors against laser radiation (laser eye-protectors) outlines appropriate eyewear requirements for protection when using lasers. The previously mentioned AS/NZS IEC 60825.14:2022 Safety of laser products Part 14: A User’s Guide (specifically Section 8.4.5 Personal Protection) also discusses the use of laser safety eyewear.”
For further information about Western Australia’s requirements, which are analagous to the treatment of vehicles, whereby you require a license to drive, and the vehicle must be registrered. Please refer to:
https://www.radiologicalcouncil.wa.gov.au/Licences
https://www.radiologicalcouncil.wa.gov.au/Registrations
NEW LASER EYEWEAR STANDARD AS 19818.1 vs AS1337.4 (EN207)
According to standards.org.au, in late 2023 AS19818.1 superseded the long standing AS1337.4 (which adopted the European Standard EN207). However as we discussed above, as of February 2026 ARPANSA is still calling up AS 13374.4. Furthermore, when arranging third party certification of our laser welding helmet in 2023, a member of the EN 19818 committee advised that we test to EN 207.
In summary: Laser welding and cleaning eyewear should be compliant with AS/NZS 1337.4 which is equivalent to European standard EN207. AS19818.1 will take over gradually, and both are valid.
WHICH LASER PROTECTIVE BARRIER AND WINDOW STANDARD TO USE?
Until now, our windows have been certified to AS/NZS 12254 (same as EN 12254). However this standard is based on 100W striking the window. For indirect reflections or welding a metre or two away this is valid. However 3000W lasers are now commonplace and we want to cover the worst case reflections at close range. For years we have performed in-house testing of our windows to AS/NZS 1337.4 (EN207), to check the penetration resistance with specular reflections at 50cm, as a worst case exposure. It is also valid to certify to AS/NZS 60825-4 which covers laser guards used to enclose the process zone of laser-processing machines.
AS/NZS 11553 REGULATES LASER MACHINE SAFETY
Laser welders, cleaners and cutters should meet AS/NZS 11553, which defines the required design standards including interlocks, emergency stops and labelling. It also requires risk assessments. Part 2 of the 11553 series governs hand held processing machines, and calls up many other standards.
The overarching and broader machine safety standard is AS/NZS 4024 which is based on EN ISO 12100.
SAFETY OF MIG OR TIG ARC WELDING VS LASER
Laser and arc welding both have light-based dangers
Note that arc welders (MIG, TIG, etc.) also present significant hazards to users and bystanders. In comparison, fibre lasers produce much less UV (ultraviolet, which is ionising radiation which means it causes cell and gene damage) than electric arc welders. However fibre lasers produce a far higher amount of near infrafed (invisible heat) light energy than arc welders. Both produce a very bright weld pool of hot, molten metal, so both need shaded lense filters to reduce the brightness, but lasers less so. Where an arc welder may need shade 12 to reduce the brightness to a comfortable level, a laser welder or cleaner usually only needs around shade 5 or 6. However some welding can be visibly very bright, so we strongly recommend the use of a welding helmet with variable shade, such as our Gen 3 laser welding helmet. Its external shade control knob is unique and ergonomic, allowing quick shade changes without the risk of removing the helmet to access internal shade controls.
Laser welders produce less fire and burn risk
When it comes to spatter and hot molten metal flying around, lasers are best by far. Lasers produce few if any sparks, and the sparks are small with very little energy. Anyone who has MIG or stick welded has been burned or had spatter fall in their boot and quickly burn into their skin. Not to mention the spatter that contributes to baldness by always managing to land on your scalp. Laser welding can produce small sparks, but far less than MIG or stick welders. Lasers also produce less bulk heat, so items are cooler to the touch. As such lasers present a much lower fire and burn hazard.
Laser welders produce less dangerous fumes than MIG or TIG
Laser welders are safer than MIG welders when it comes to welding fumes. MIG produce a lot of tiny airborne soot, and fume such as vaporised metal and metal ions. These are inurious over time when inhaled, and the danger is becoming more well known. The most harmful types are Chrome and Nickel based from oxidation (the black stain on stainless steel when MIG or TIG welded), and the Chrome is often present as hexavalent chrome (Cr6+) which is a known carcinogen.
Laser welders input about one quarter of the heat of arc welders, as demonstrated by the reduced distortion and very small heat affected zones.
Laser welds don’t need grinding, so reduce dust hazards
Most laser welds require no, or very minimal grinding. In comparison, MIG welds (and my TIG welds, if you’ve ever see them!) require a lot of grinding to achieve a professional finish. Grinding produces a lot of metal and abrasive dust, which is very hazardous to lungs.
Laser welders use less chemicals than MIG or TIG
Due to the smaller heat input, many laser welds on stainless steel do not even require cleaning. In general, silver, yellow or straw colour on stainless steel is considered non corrosive and does not require cleaning. In contrast, most MIG welds will require pickling (which uses dangerous hydrofluoric acid) or at least TIG brushing which uses a milder acid. If the welds are ground or brush to remove stain, once again laser welding is safer because these processes also produce dust and the risk of personal injury.
Laser welders produce less stress and coronary artery disease
Stress is a killer. As a business owner in the manufacturing industry I can assure you a laser welder reduces management stress because:
(a) Laser welding can be done with less skilled workers. This saves on payroll, training, recruiting and headaches, particularly where good workers are hard to find and expensive to hire.
(b) Laser welding is much faster and requires less rework and finishing. This saves a lot of money and increases throughput which also means less overhead cost per job. One business owner called to report their 60 minute TIG job was now taking 4 minutes with our G5 laser welder. That is 15 times faster, and they welds were neater and had full penetration. Your mileage may vary, but you can expect to weld at least 5x as fast as TIG.
(c) Laser welders use about 1/4 the electricity and 1/3 the gas, because you are welding so much faster than TIG.
HOW TO REDUCE THE LASER SAFETY RISK?
Simply put, an enclosed area is required with signage and correctly rated laser glasses. People must not be able to see in or enter unless wearing correctly rated laser eyewear. A light safe enclosure with warning light and interlock on the door is required for complete compliance.
Fortunately laser light from our laser welders is focused, so it expands and weakens. The further away you are from the laser, the lower the light intensity. Laser intensity drops exponentially as you move away, but at closer distances such as a workshop anyone’s eyes could be damaged, even by reflections.
The Australian Standards AS60825.1 and .14 should be followed, but some practical things to factor into your safety plan are:
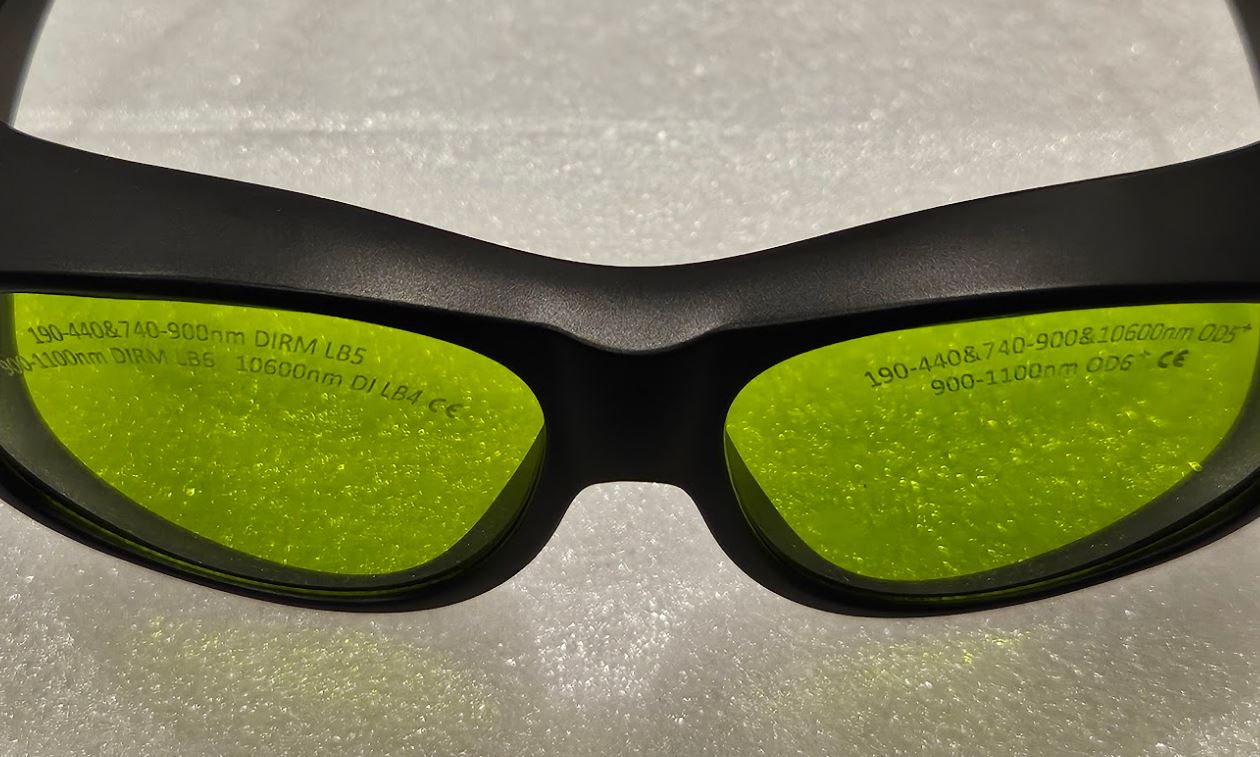
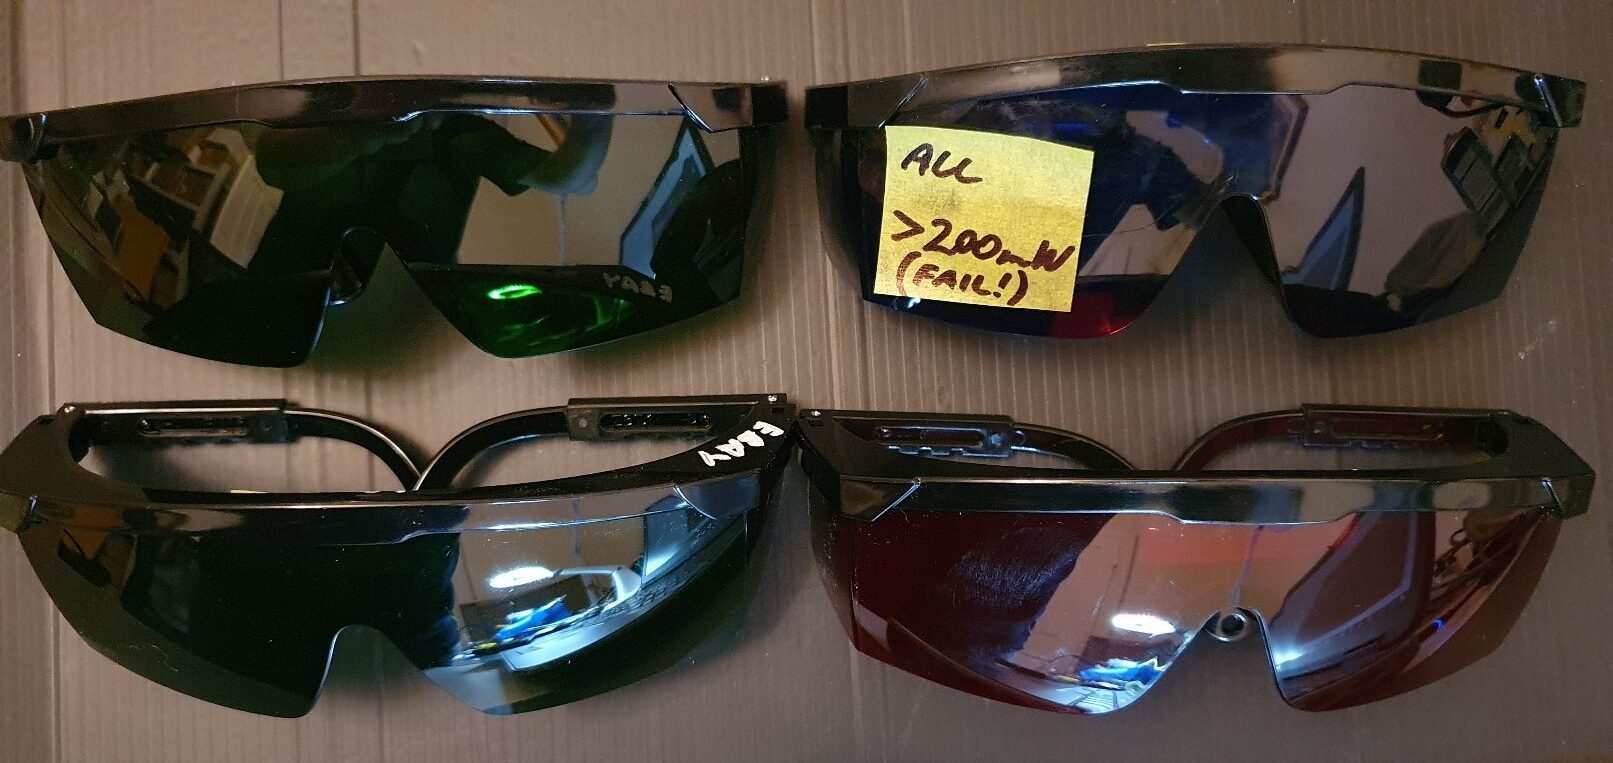
- Anyone in the enclosure must be using correctly rated laser eye protection. This means CE marking and D LB6 (or OD6) or higher for at least the range of wavelengths 1050-1090nm, or whatever wavelength your machine is rated at. Anyone within 6 metres of the welding must wear that eyewear and a laser welding helmet.
- No one can be near the exit path of the laser (where a lot of the laser beam energy bounces off the surface at the same angle it hits the surface). Similar to a shooting range, never be out in front where the guns are pointed…
- Use tall, dull black surrounds and panelling to absorb the laser light and avoid reflections. Black powder coated aluminium is the best material for an enclosure, at least 1.5mm thick. Cement sheet is also OK. Other materials will work, but can be a fire risk in the worst case.
- Avoid anyone walking in unaware. Use signage to AS1319, such as the sign we provide with every machine, and wire up the provided door interlock circuit to a door switch which opens when the door starts to open.
- If the room or door has windows, use approved laser rated viewing windows, ideally rated AB 6 to EN 12254, or D LB 6 or even OD6 or numerically higher. Place correctly rated glasses on the entry door for anyone about to enter the area, with signage.
- Use bright work lighting. This makes it easy to see what you are welding, and keeps the iris small, in the “bright sunshine” mode which is our eyes’ natural defence to minimise solar radiation damage.
- The molten welding pool is bright, and bright visible light can cause eye damage too. You will want to weld with an arc welding (Infrared blocking) filter shade around 4 or 5 and the glasses of point 1 for maximum safety.
- Laser welders have a safety feature that only enables the laser to fire if the nozzle is in electrical contact with the sensing clamp (which is normally clipped to the steel welding table, or directly to the workpiece). If you lay the gun (welding head) on the metal workbench, or the gun can slip onto it, the gun is then enabled and could fire if it hits the trigger/s. This CAN happen, so please be sure to position the head on a non-conductive, non-slip surface, ideally leather or rubber, near but insulated from the welding table. And of course, don’t clip the sensing clamp to the welding head as that leaves the laser enabled and vulnerable to bumping the trigger button.
- Don’t weld towards the door. Where possible, weld so the reflected laser light/radiation goes into a corner. It then has to reflect from at least two walls before it can head towards personnel. Each time it strikes a surface the radiation is absorbed and scattered to some degree. The darker and duller/textured the surface, the more the laser is absorbed and scattered.